An LED lighting sample is useful only when its exact identity, configuration, test conditions and acceptance criteria are controlled. A visually acceptable unit can still differ from the quotation, drawing, driver, optics, firmware, label, packaging or installation parts intended for production.
Freeze the sample identity before testing, separate observations from measurements and formal evidence, record every result and deviation, and approve only the configuration and revision actually evaluated. A sample approval is a design decision; production consistency, lot inspection and change control remain separate controls.
Freeze the Sample Identity
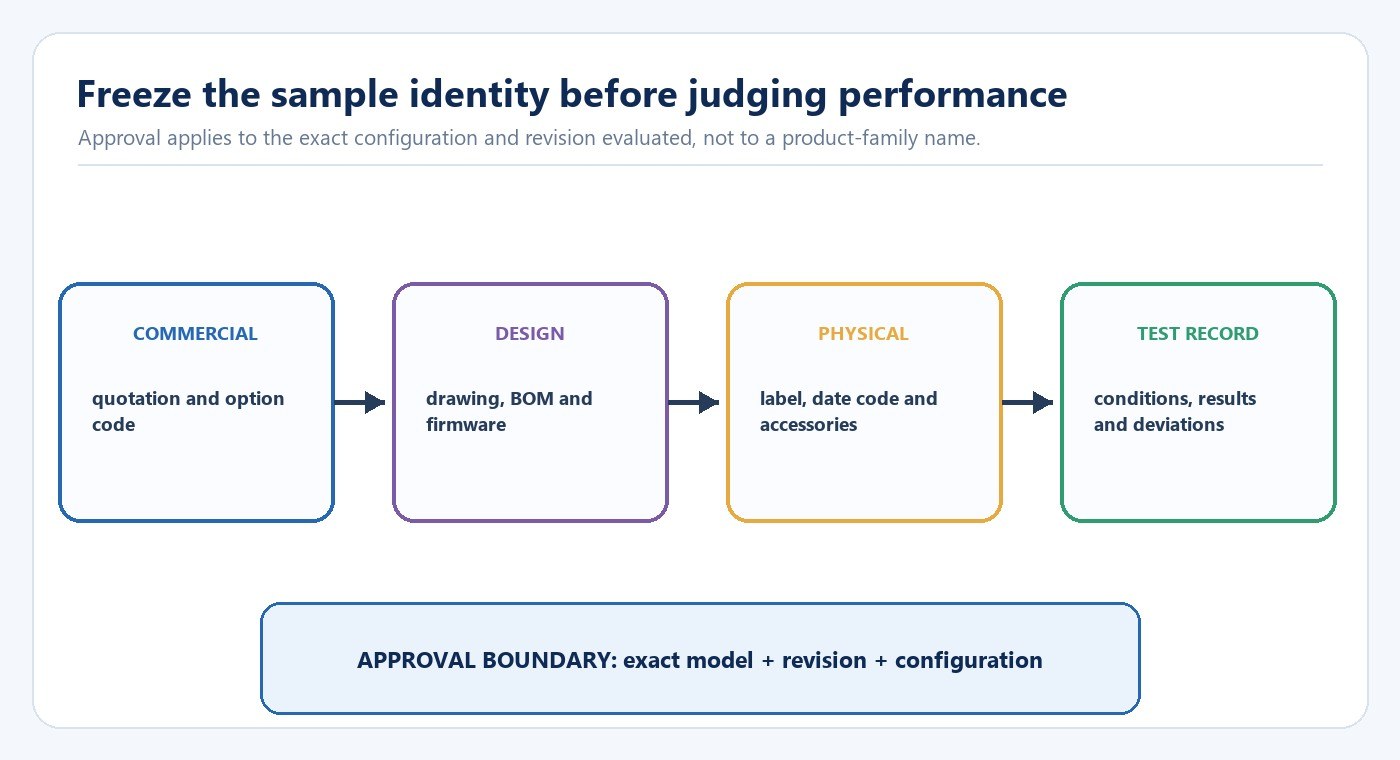
Photograph the outer carton, product labels, accessories and complete unit. Record supplier, model, revision, date code, rated input, CCT, finish, driver, optic, control option, mounting parts and production-intent status. Reconcile these fields with the quotation, datasheet, drawing and bill-of-material reference.
| Identity field | Compare against | Risk if omitted |
|---|---|---|
| Model and option code | Quotation, label and datasheet | Wrong configuration approved |
| Design revision | Drawing, BOM, firmware and instructions | Test result applied to a changed design |
| Critical components | Driver, LED board, optics and controls | Performance or evidence no longer matches |
| Accessories and packaging | Parts list, artwork and installation plan | Site or market package remains incomplete |
Mark the sample and its photographs with one review identifier. If a replacement sample arrives, do not silently overwrite the first record; state which checks were repeated and which evidence remains applicable.
Separate the Four Evidence Types
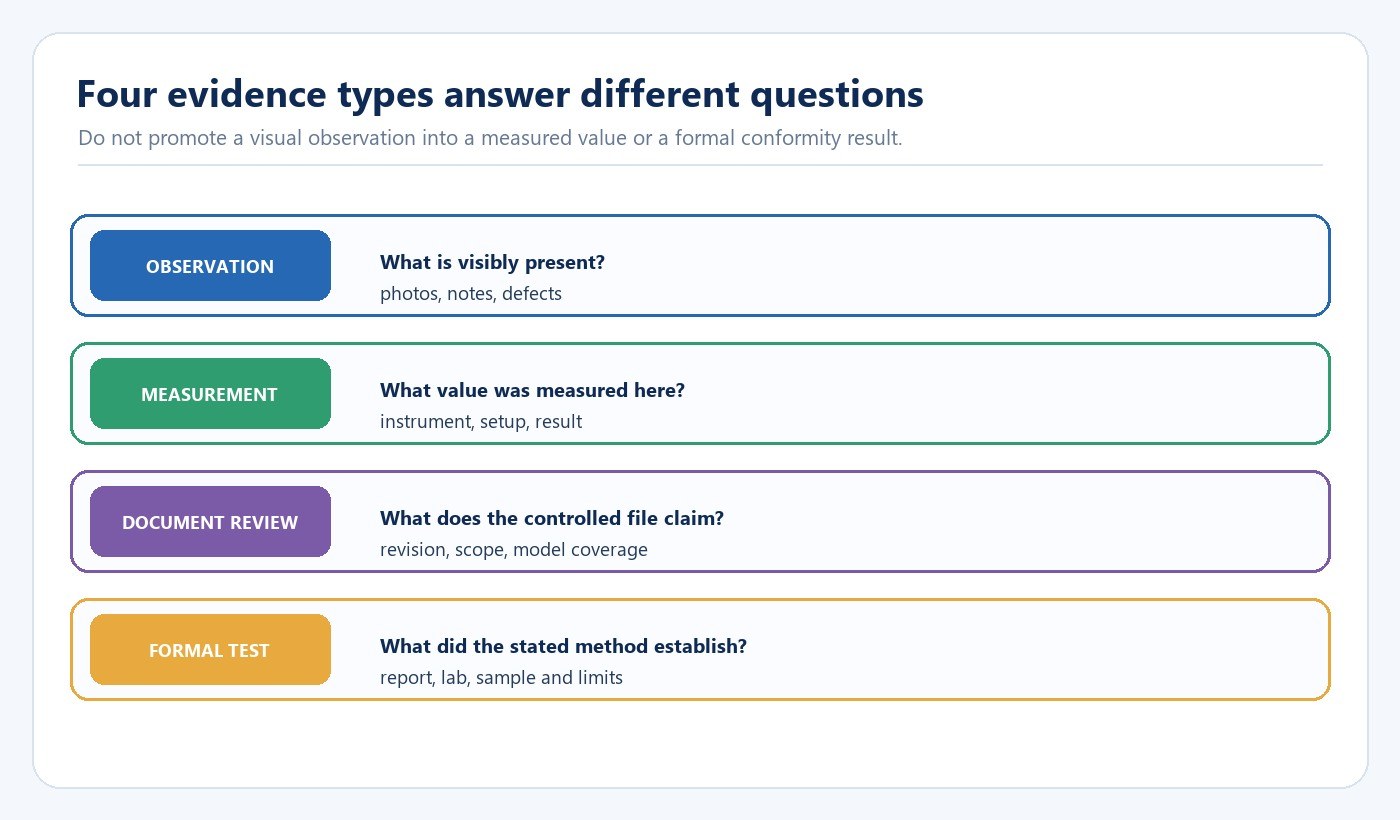
An observation can identify finish defects, loose parts, incomplete labels or inconsistent assembly. A measurement adds a defined instrument, setup, operating condition and value. A document review checks revision, scope, issuing organization and model coverage. A formal report states the method, sample, limits and results under its own scope.
The International Electrotechnical Commission’s IEC 60598-1:2024 specifies general safety requirements and tests for luminaires. A buyer’s bench review may reveal mismatches, but it does not reproduce a complete conformity assessment. Ask for the applicable report or certificate, issuing body, model coverage and revision, then verify that the physical sample matches that evidence.
Do not infer an ingress rating from a gasket, protective-earth compliance from one visible lead, or complete-system compatibility from a familiar driver label. Record the level of evidence actually available.
Check Construction and Installation Reality
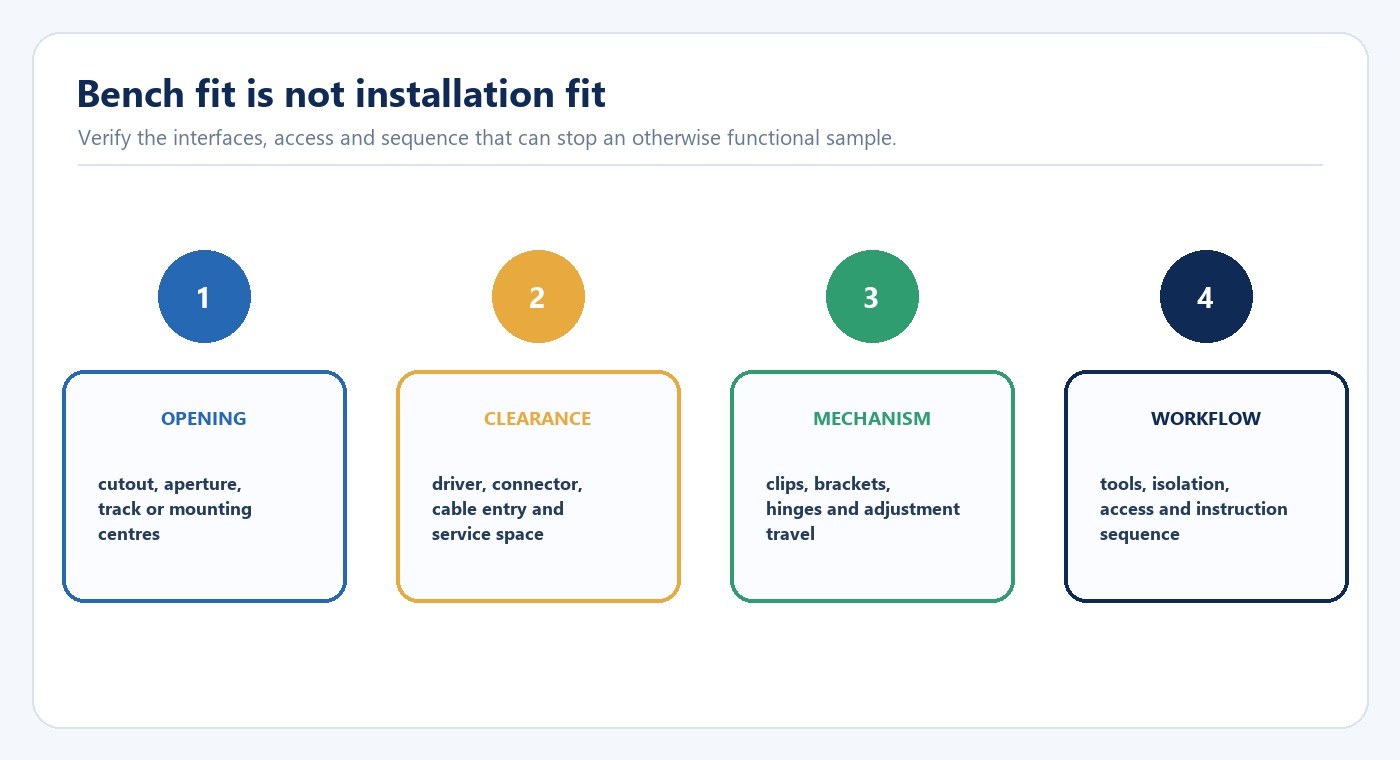
Confirm dimensions at interfaces that control fit: cutout, aperture, mounting centres, track profile, bracket travel, cable entry, connector clearance and service space. Operate clips, hinges and adjustment points. Inspect sharp edges, exposed conductors, strain relief, fastener engagement, finish consistency and parts that could loosen.
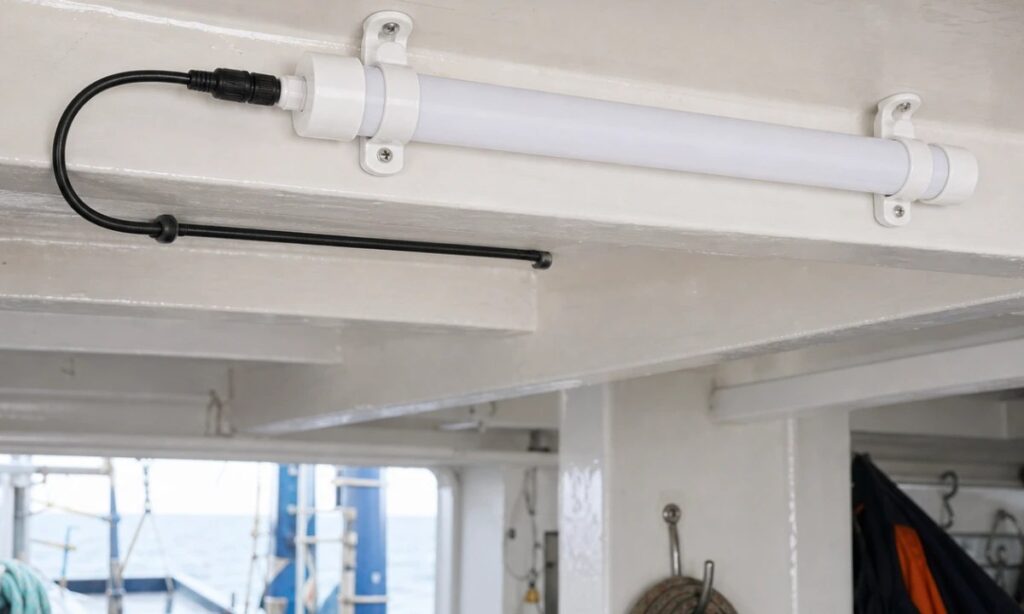
Use the intended ceiling, track, junction box, shelf or mock surface where practical. Record tools, sequence, isolation, access and conflicts with the instruction. A unit that works on a bench can still fail because the driver cannot pass through the opening, the bracket cannot rotate, the connector lacks clearance or servicing damages the finish.
| Interface | Practical check | Acceptance evidence |
|---|---|---|
| Mounting geometry | Measure actual opening, centres, depth and travel | Dimensions and installation photographs |
| Cable and connector | Route without crushing, sharp bends or inaccessible joints | Final route and strain-relief record |
| Adjustment and service | Operate through intended range and removal sequence | Tools, clearances and instruction match |
| Finish and assembly | Compare visible surfaces, gaps and fasteners | Defect photographs and disposition |
Evaluate Light, Electrical and Control Behavior
Record supply voltage, ambient condition, warm-up time, control equipment, instrument identity and measurement geometry. Compare input power, startup, abnormal noise or heat, output, distribution, color and flicker evidence at the same operating point.
For dimming, check startup, shutoff, minimum stable level, visible stepping, flicker and the named dimmer or control system. For sensors and connected products, test the actual sequence, detection boundary, timing, failure state and commissioning controls rather than a single on/off demonstration.
Visual comparison is useful for beam shape, glare, color consistency and surface defects, but it is not a calibrated photometric or electrical test. The LED flicker, power factor and THD checklist explains why electrical and temporal-light metrics need separate conditions and limits.
Match the Sample to Documents and Market Scope
Check that model numbers, ratings, labels, warnings, installation instructions, packaging artwork and declarations tell the same story. A report for a related family may or may not cover the submitted option; request the model relationship and controlled differences.
The LED product compliance document checklist provides a file-level review, while the OEM and ODM RFQ guide helps freeze the requested configuration before the sample is built.
| Document | Match to sample | Typical mismatch |
|---|---|---|
| Datasheet and drawing | Model, input, dimensions, options and revision | Quotation option absent from drawing |
| Test report or certificate | Model coverage, construction and market scope | Similar family used without relationship evidence |
| Installation instruction | Wiring, mounting, warnings and accessories | Instruction describes another architecture |
| Carton and product label | Ratings, marks, model and traceability | Artwork revision lags behind approved product |
Use First-Party Inspection as Traceable Context
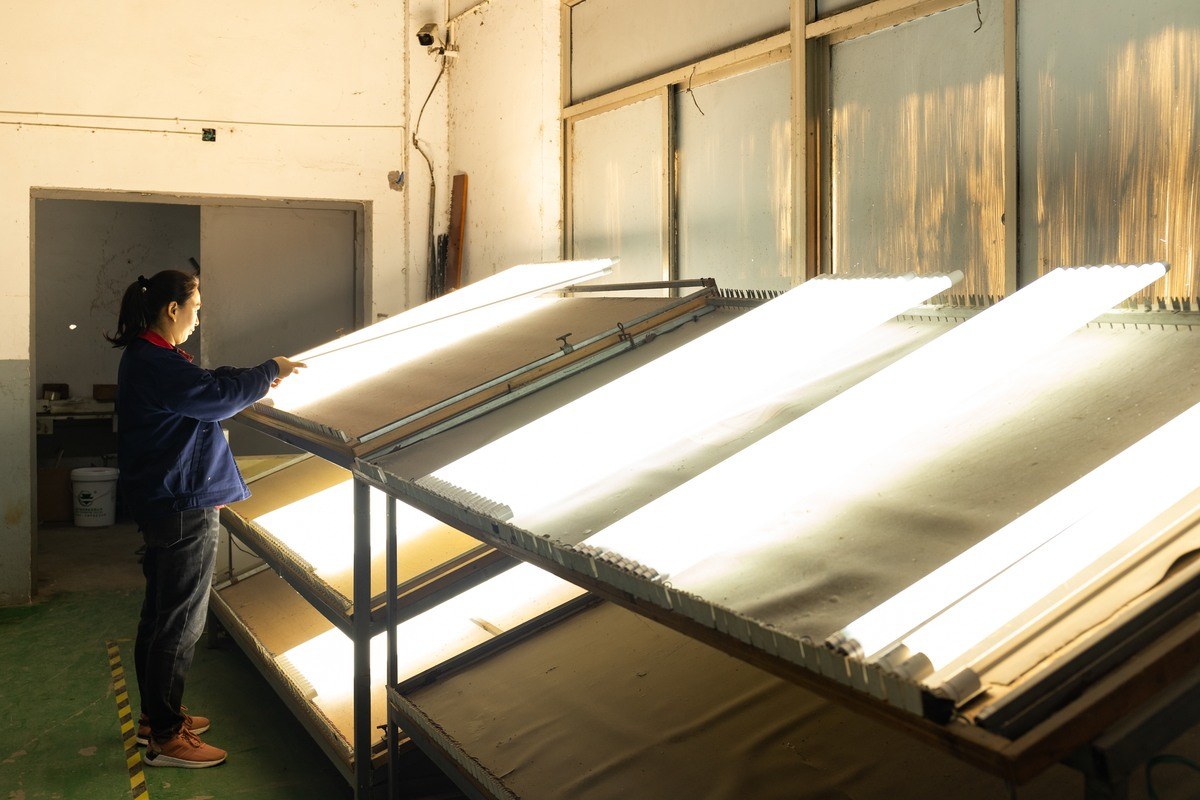
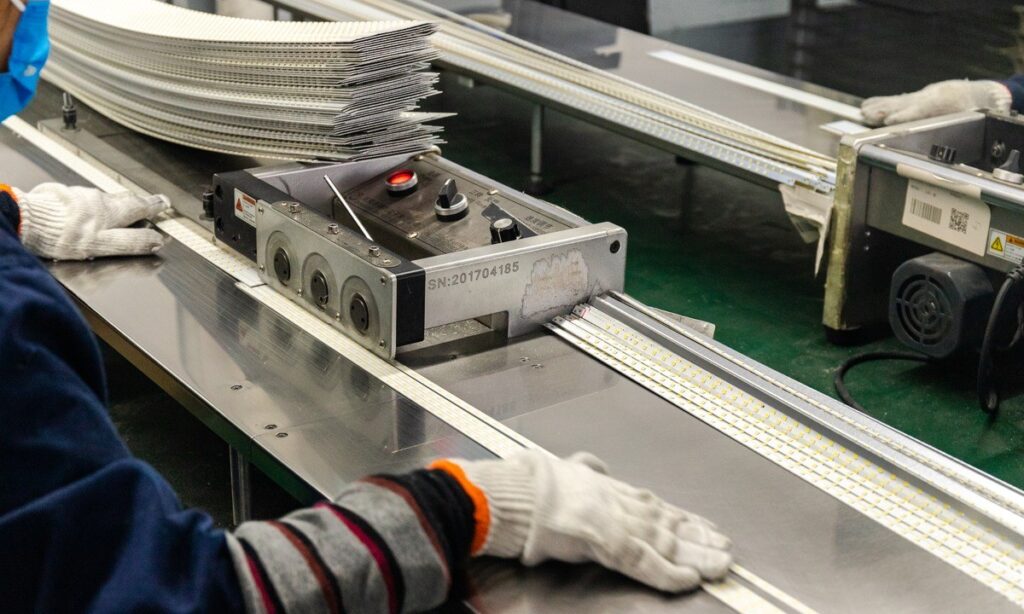
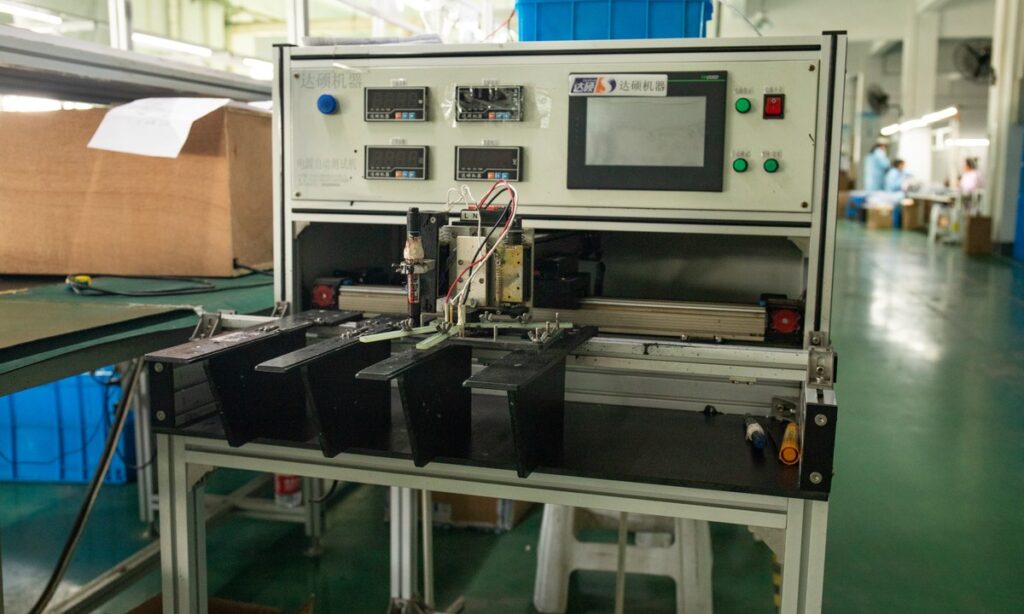
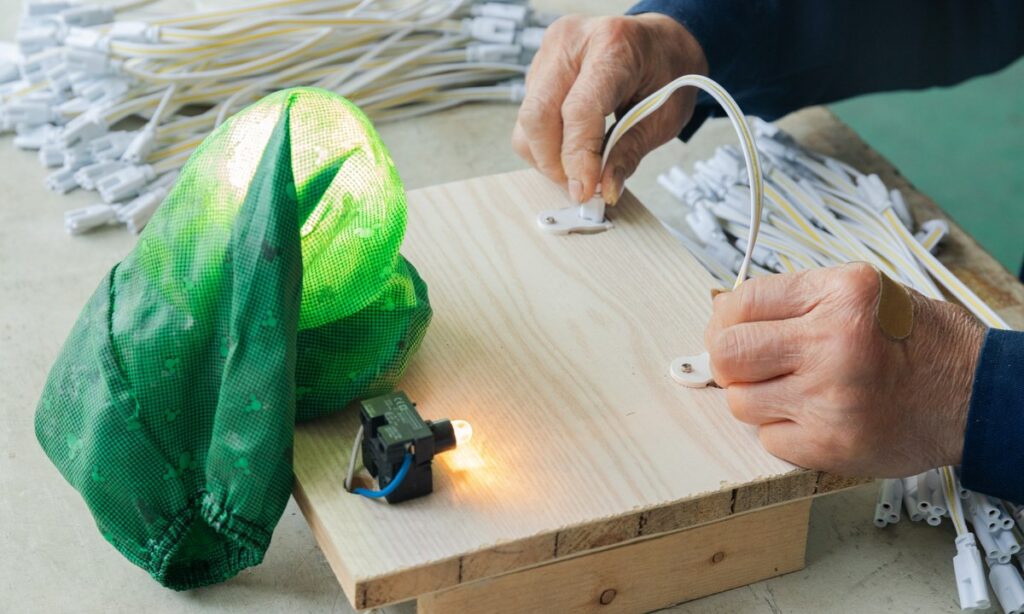
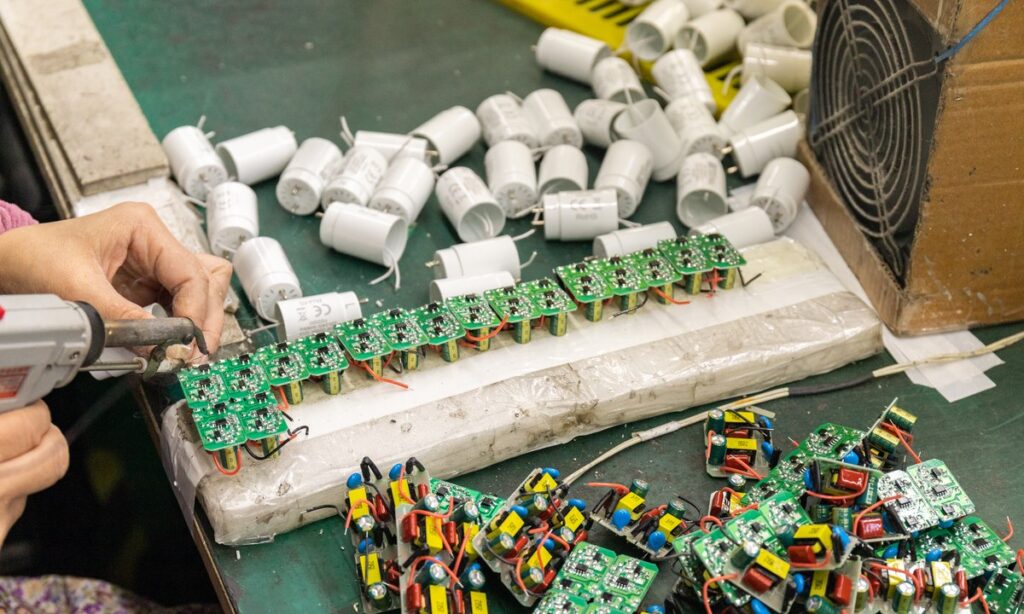
An in-process photograph can show where inspection occurs, but the decision record should carry the sample or lot identity, requirement, method, result, inspector and disposition. The factory audit checklist extends the review from one sample to process controls, calibration, change control and traceability.
Close Deviations Before Approval
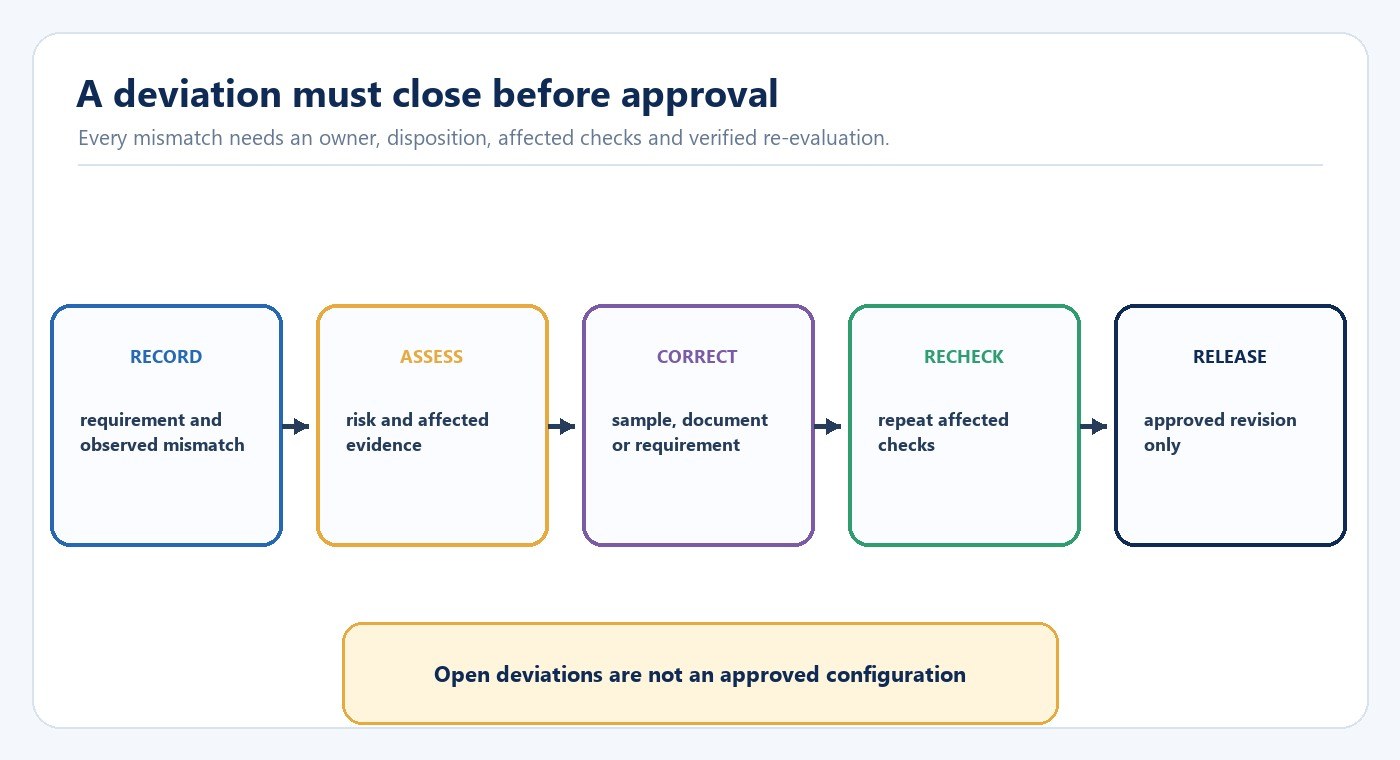
For every deviation, identify the requirement, observed condition, owner, risk, proposed disposition and affected checks. “Accept as is” still needs authorized reasoning and a defined scope. A corrected drawing does not prove the sample changed; a corrected sample does not prove the production document changed.
Approve only after the record shows what was corrected and what was rechecked. Tie the final approval to the released sample revision, design files and permitted tolerances.
Keep Sample Approval Separate from Lot Acceptance
A development or pre-production sample supports design approval. It does not establish that every production unit matches. The International Organization for Standardization’s ISO 2859-1:2026 defines AQL-indexed sampling schemes for lot-by-lot inspection by attributes, while ISO 28590:2017 introduces the ISO 2859 family and selection of an inspection system.
The buyer still needs to define lot formation, inspection level, defect classes, AQLs, switching rules and handling of critical requirements. Sampling does not make every nonconformity acceptable, and it does not replace safety or legal controls.
Sample Release Checklist
Before approval, confirm:
- Model, revision, options and production-intent status are explicit.
- Quotation, drawing, datasheet, BOM reference and instructions use controlled revisions.
- Mechanical interfaces were checked in the intended installation condition.
- Operation was evaluated at recorded supply, ambient and control conditions.
- Photometric and electrical results state method and operating point.
- Compliance documents match model, configuration, market and revision.
- Every deviation has an owner, disposition and completed recheck.
- The approved sample is tied to the production specification and tolerances.
- Lot inspection and critical defect controls are defined separately.
- Component and document changes require an impact review before release.
Review relevant New Lights product families, align the production boundary with the lighting maintenance and spare-parts guide, and send the requirement matrix through the project enquiry form.
Frequently Asked Questions
Can one approved sample release mass production?
Only if the contract defines that gate and all required evidence is complete. Production consistency, lot inspection and change control remain separate.
Should a buyer open the luminaire?
Only through an agreed safe method. Opening can affect seals, warranty or evidence status. Request a designated teardown sample when internal review is needed.
What if the sample differs from the report or drawing?
Stop approval for that configuration. Record the mismatch, obtain corrected evidence or a corrected sample, and repeat every affected check.
Editorial Sources
- International Electrotechnical Commission, “IEC 60598-1:2024”: https://webstore.iec.ch/en/publication/66620
- International Organization for Standardization, “ISO 2859-1:2026”: https://www.iso.org/standard/85464.html
- International Organization for Standardization, “ISO 28590:2017”: https://www.iso.org/standard/64622.html